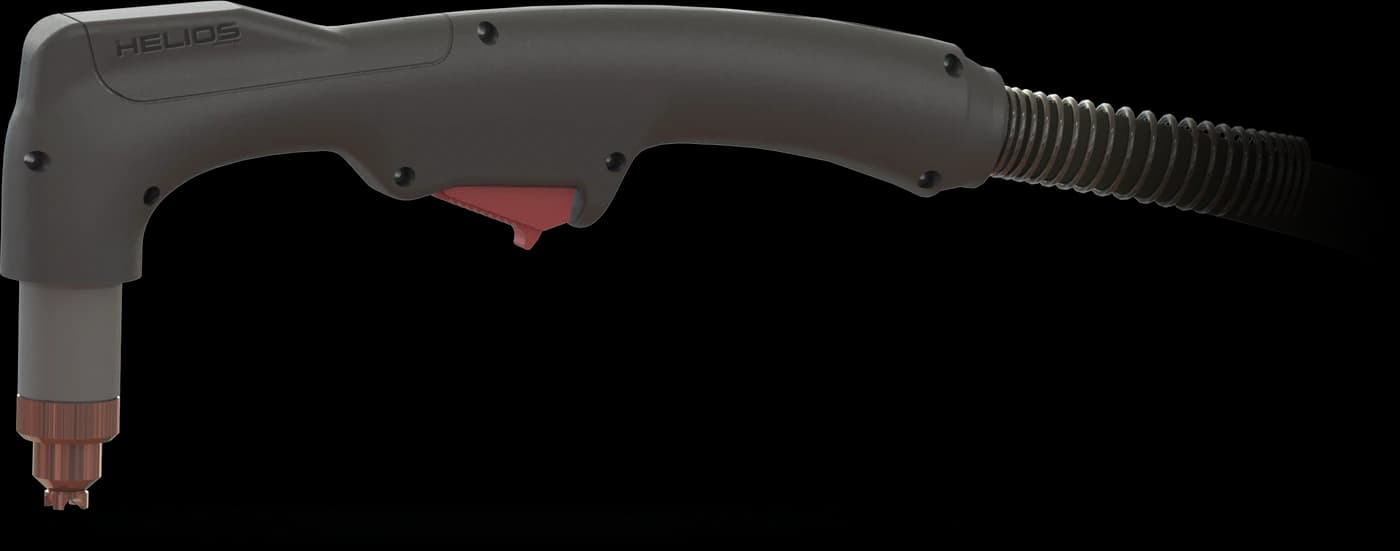
SCORPION CUT HT-120
120 A plasma cutting torch
Industrial cutting. Severs up to 50 mm of steel.
- 120A
- Max. current
- 32mm
- Recommended cut
- 50mm
- Severance cut
01 / Overview
Industrial cutting. Severs up to 50 mm of steel.
120 A at 60 % duty cycle, with a 40 to 120 A current range. Pilot arc ignition between electrode and tip, with no high frequency.
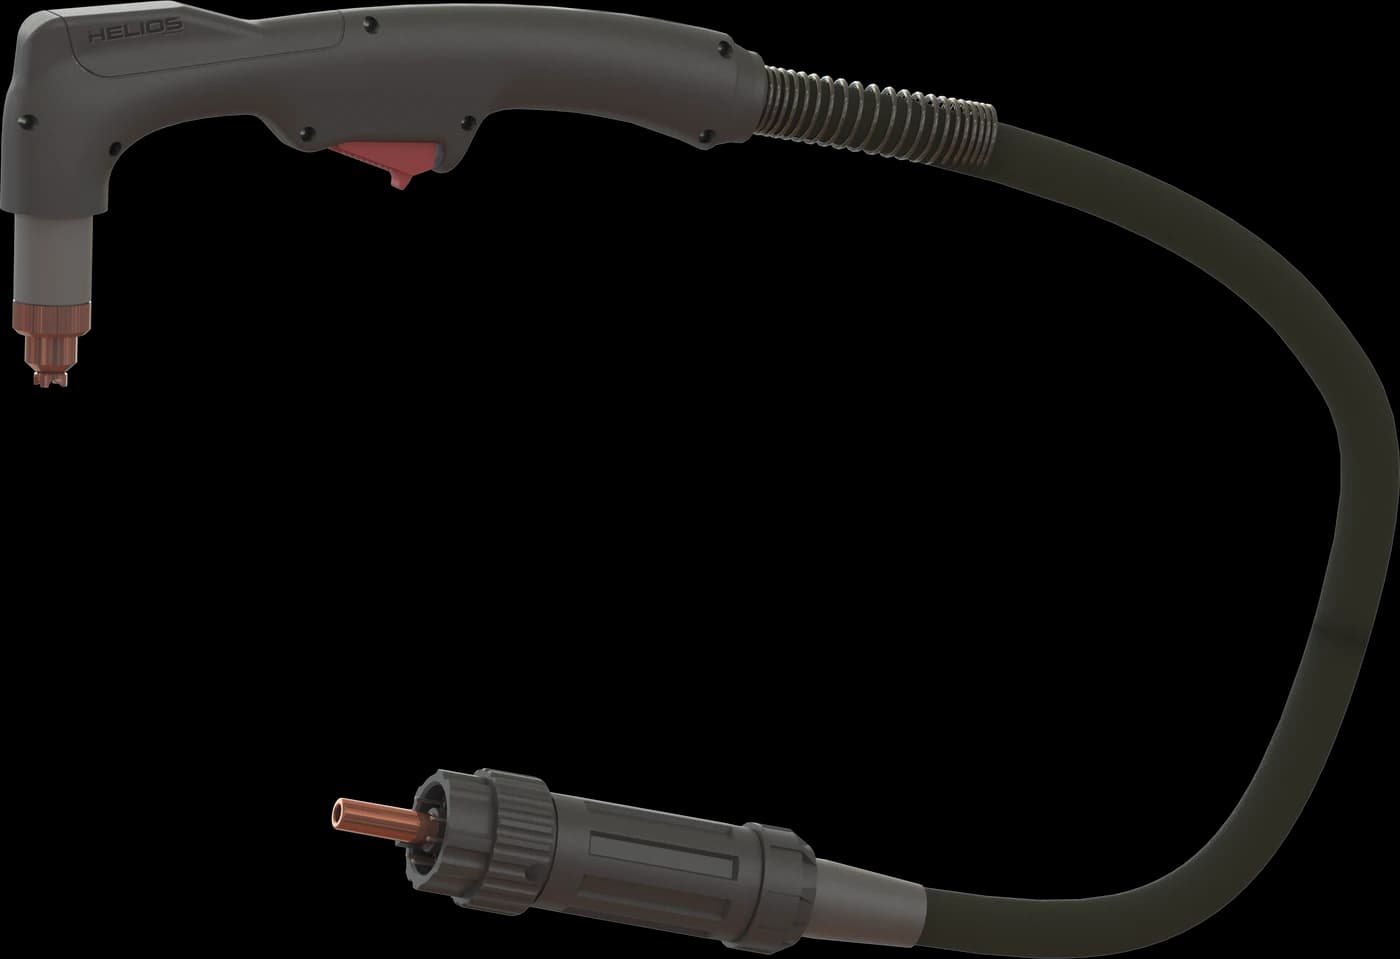
Recommended cut of 32 mm (1-1/4 in) at 500 mm/min (20 in/min) and 38 mm (1-1/2 in) at 250 mm/min (10 in/min); severance cut (manual cutting) of 50 mm (2 in) at 125 mm/min (5 in/min). Runs on compressed air or nitrogen at 5.5 – 6 bar (72 – 80 psi) and 250 l/min, with a 6 or 12 m (20 or 40 ft) coaxial cable and a central adaptor to connect to the plasma power source.
Figures for guidance only: cutting capacity and speed vary depending on the plasma power source and on air quality and flow.
Model
SCORPION CUT HT-120
Reference
HPT-P12-060 · HPT-P12-120
Family
Torches & accessories
Sheet / Rev.
01 / A
Data from the official HELIOS datasheet. Subject to continuous improvement.
02 / Technical sheet
Technical sheet
Current range
40–120A
60%
Duty cycle
Electrical
2- Amperage range
- 40 – 120 A
- Duty cycle
- 60 % (120 A)
Process & control
11- Processes
- Plasma
- Ignition
- Pilot arc
- Recommended cut
- 32 – 38 mm (1-1/4 – 1-1/2")
- Severance cut
- 50 mm (2")
- Cutting speed · 32 mm
- 500 mm/min (20 in/min)
- Cutting speed · 38 mm
- 250 mm/min (10 in/min)
- Cutting speed · 50 mm
- 125 mm/min (5 in/min)
- Cutting gas
- Air / N₂
- Gas pressure
- 5.5 – 6 bar (72 – 80 psi)
- Gas flow
- 250 l/min
- Post-flow
- 45 s
Physical & environment
1- Cable length
- 6 m (20 ft) · 12 m (40 ft)
Other data
2- Cable
- Coaxial
- Connectors
- Central adaptor
Cutting curve
Thickness and cutting speed
Mild steel · shielded machine cutting · 105 A plasma power source
With a 105 A plasma power source
- Current
- 40 – 100 A
- Duty cycle
- 80 % (100 A)
- Tip and shield
- 105 A
- Torch-to-work distance
- 3.2 mm
- Initial pierce height
- 6.4 mm (200 %)
- Air flow (hot / cold)
- 217 / 250 l/min
iReference data with a 105 A plasma power source (shielded machine cutting, mild steel): not the maximum capacity of the torch. Actual speed varies depending on the plasma power source, on air quality and flow, and on the settings.
| Thickness · mm | 6 | 8 | 10 | 12 | 16 | 20 | 25 | 30 | 32 | 35 | 40 |
|---|---|---|---|---|---|---|---|---|---|---|---|
| Best quality · mm/min | 4140 | 3140 | 2260 | 1690 | 1060 | 780 | 550 | 370 | 350 | 290 | 190 |
| Arc voltage · V | 144 | 145 | 145 | 145 | 149 | 152 | 159 | 162 | 166 | 168 | 173 |
| Production · mm/min | 5090 | 3870 | 2790 | 2060 | 1310 | 940 | 580 | 410 | 370 | 320 | 210 |
| Arc voltage · V | 145 | 145 | 145 | 148 | 149 | 152 | 158 | 161 | 161 | 165 | 170 |
| Pierce delay · s | 0.5 | 0.75 | 0.75 | 0.75 | 1 | 1 | Edge | Edge | Edge | Edge | Edge |
Spare parts
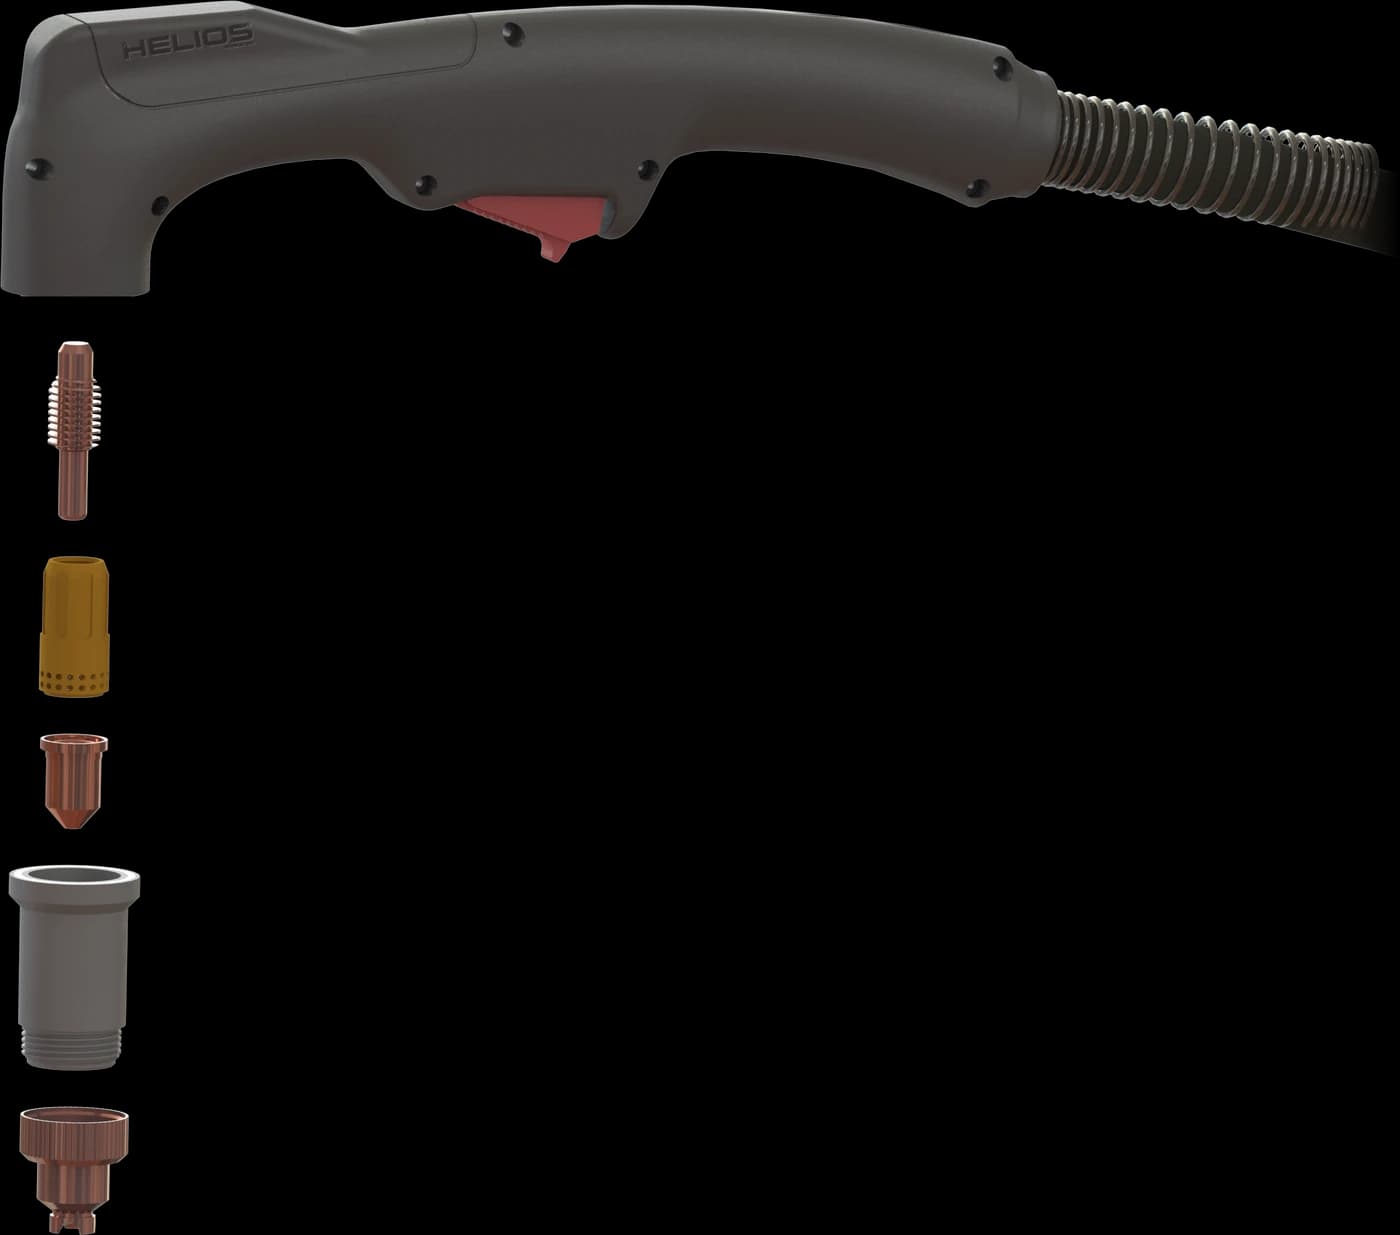
Exploded view & spare parts
Position number in the drawing, HELIOS part number and description of each part.
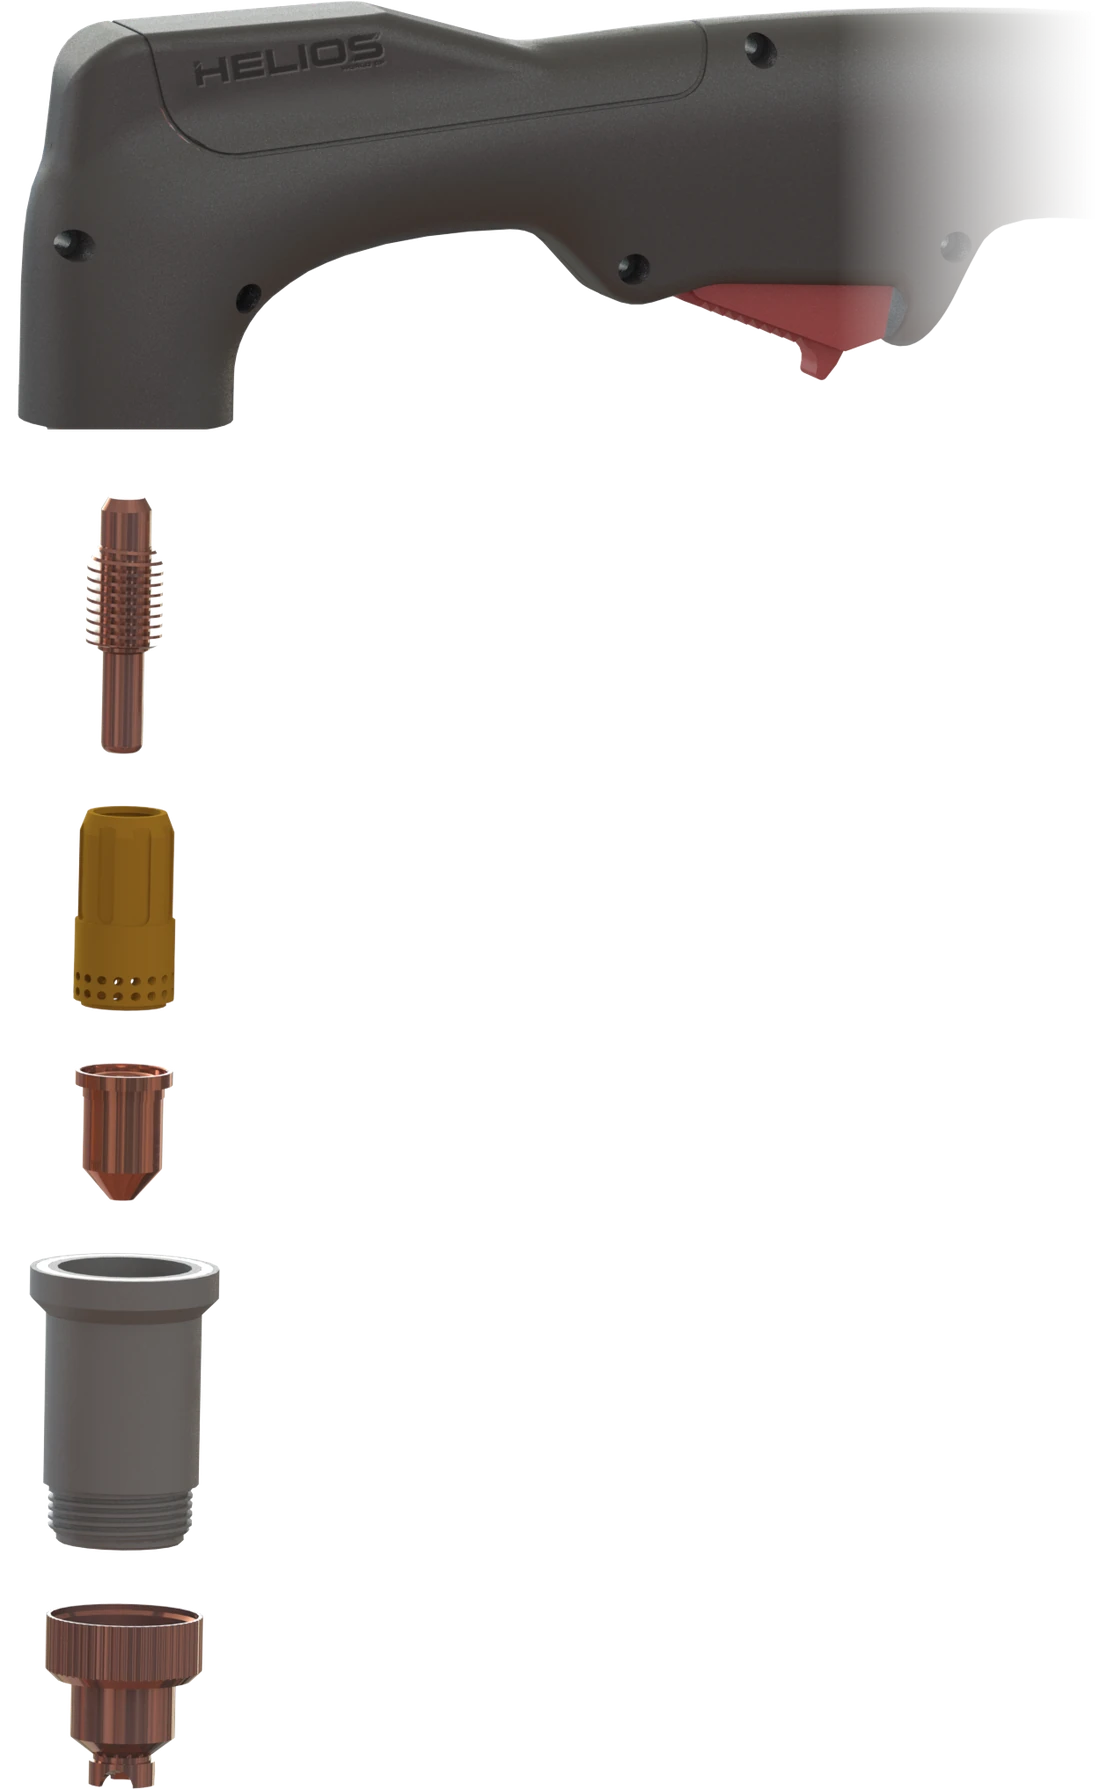 12345
| Pos. | Part no. | Description |
|---|---|---|
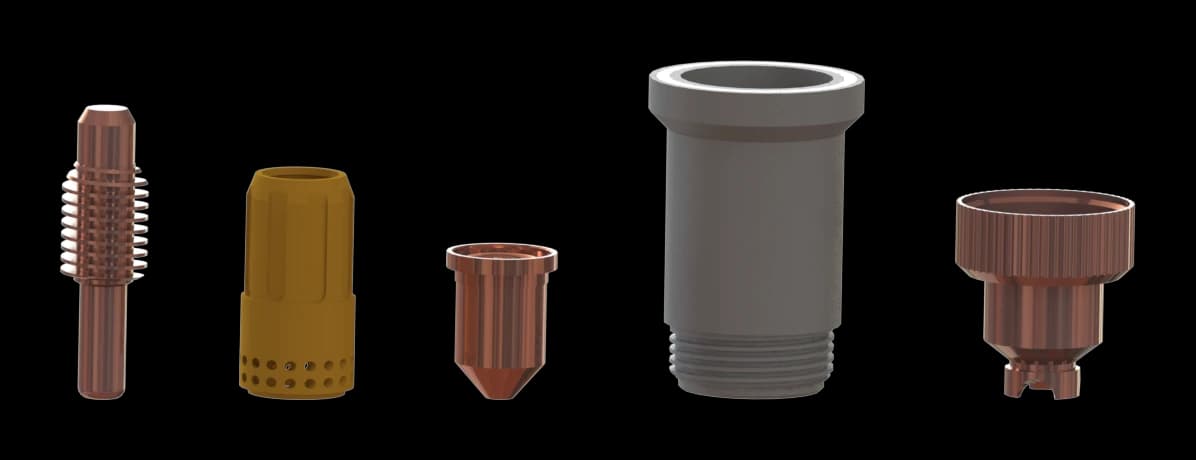
| 1 | HPP-P12-E01 | Electrode |
| 2 | HPP-P12-D01 | Swirl ring (gas distributor) |
| 3 | HPP-P12-T01 | Cutting tip 105 A (nozzle) |
| 4 | HPP-P12-C01 | Retaining cup |
| 5 | HPP-P12-S01 | Drag shield 105 A |
| Part no. | Complete torches | |
|---|---|---|
| HPT-P12-060 | Complete torch 6 m (20 ft) | |
| HPT-P12-120 | Complete torch 12 m (40 ft) |
PDF datasheet
Take the full datasheet with you
A PDF with the photo, every figure and this machine's QR code, in HELIOS's own design and with its own document ID so you always know which revision you are holding.